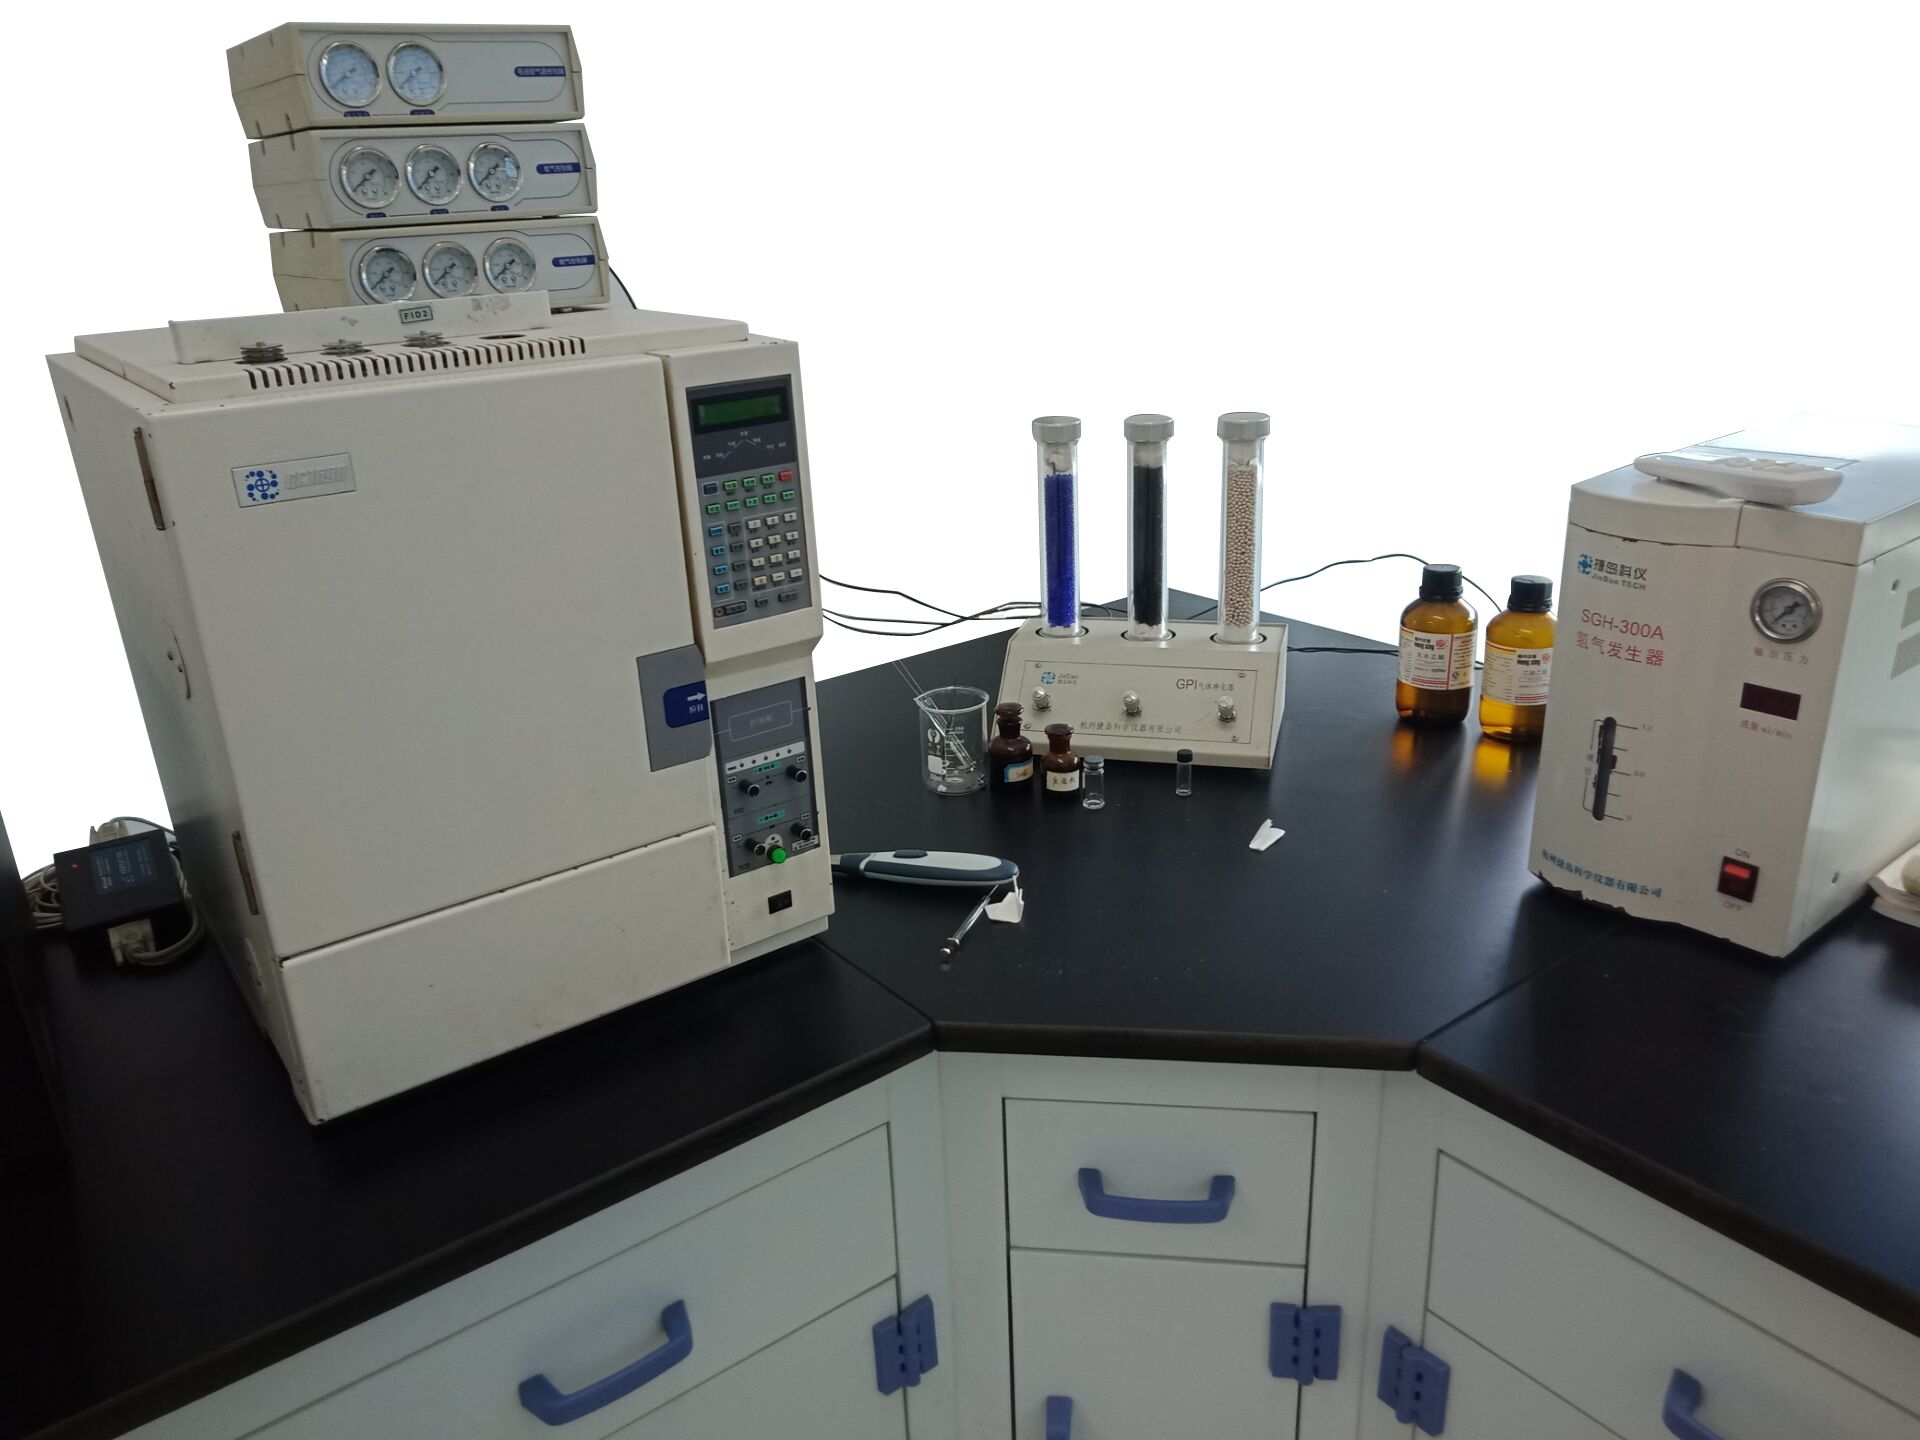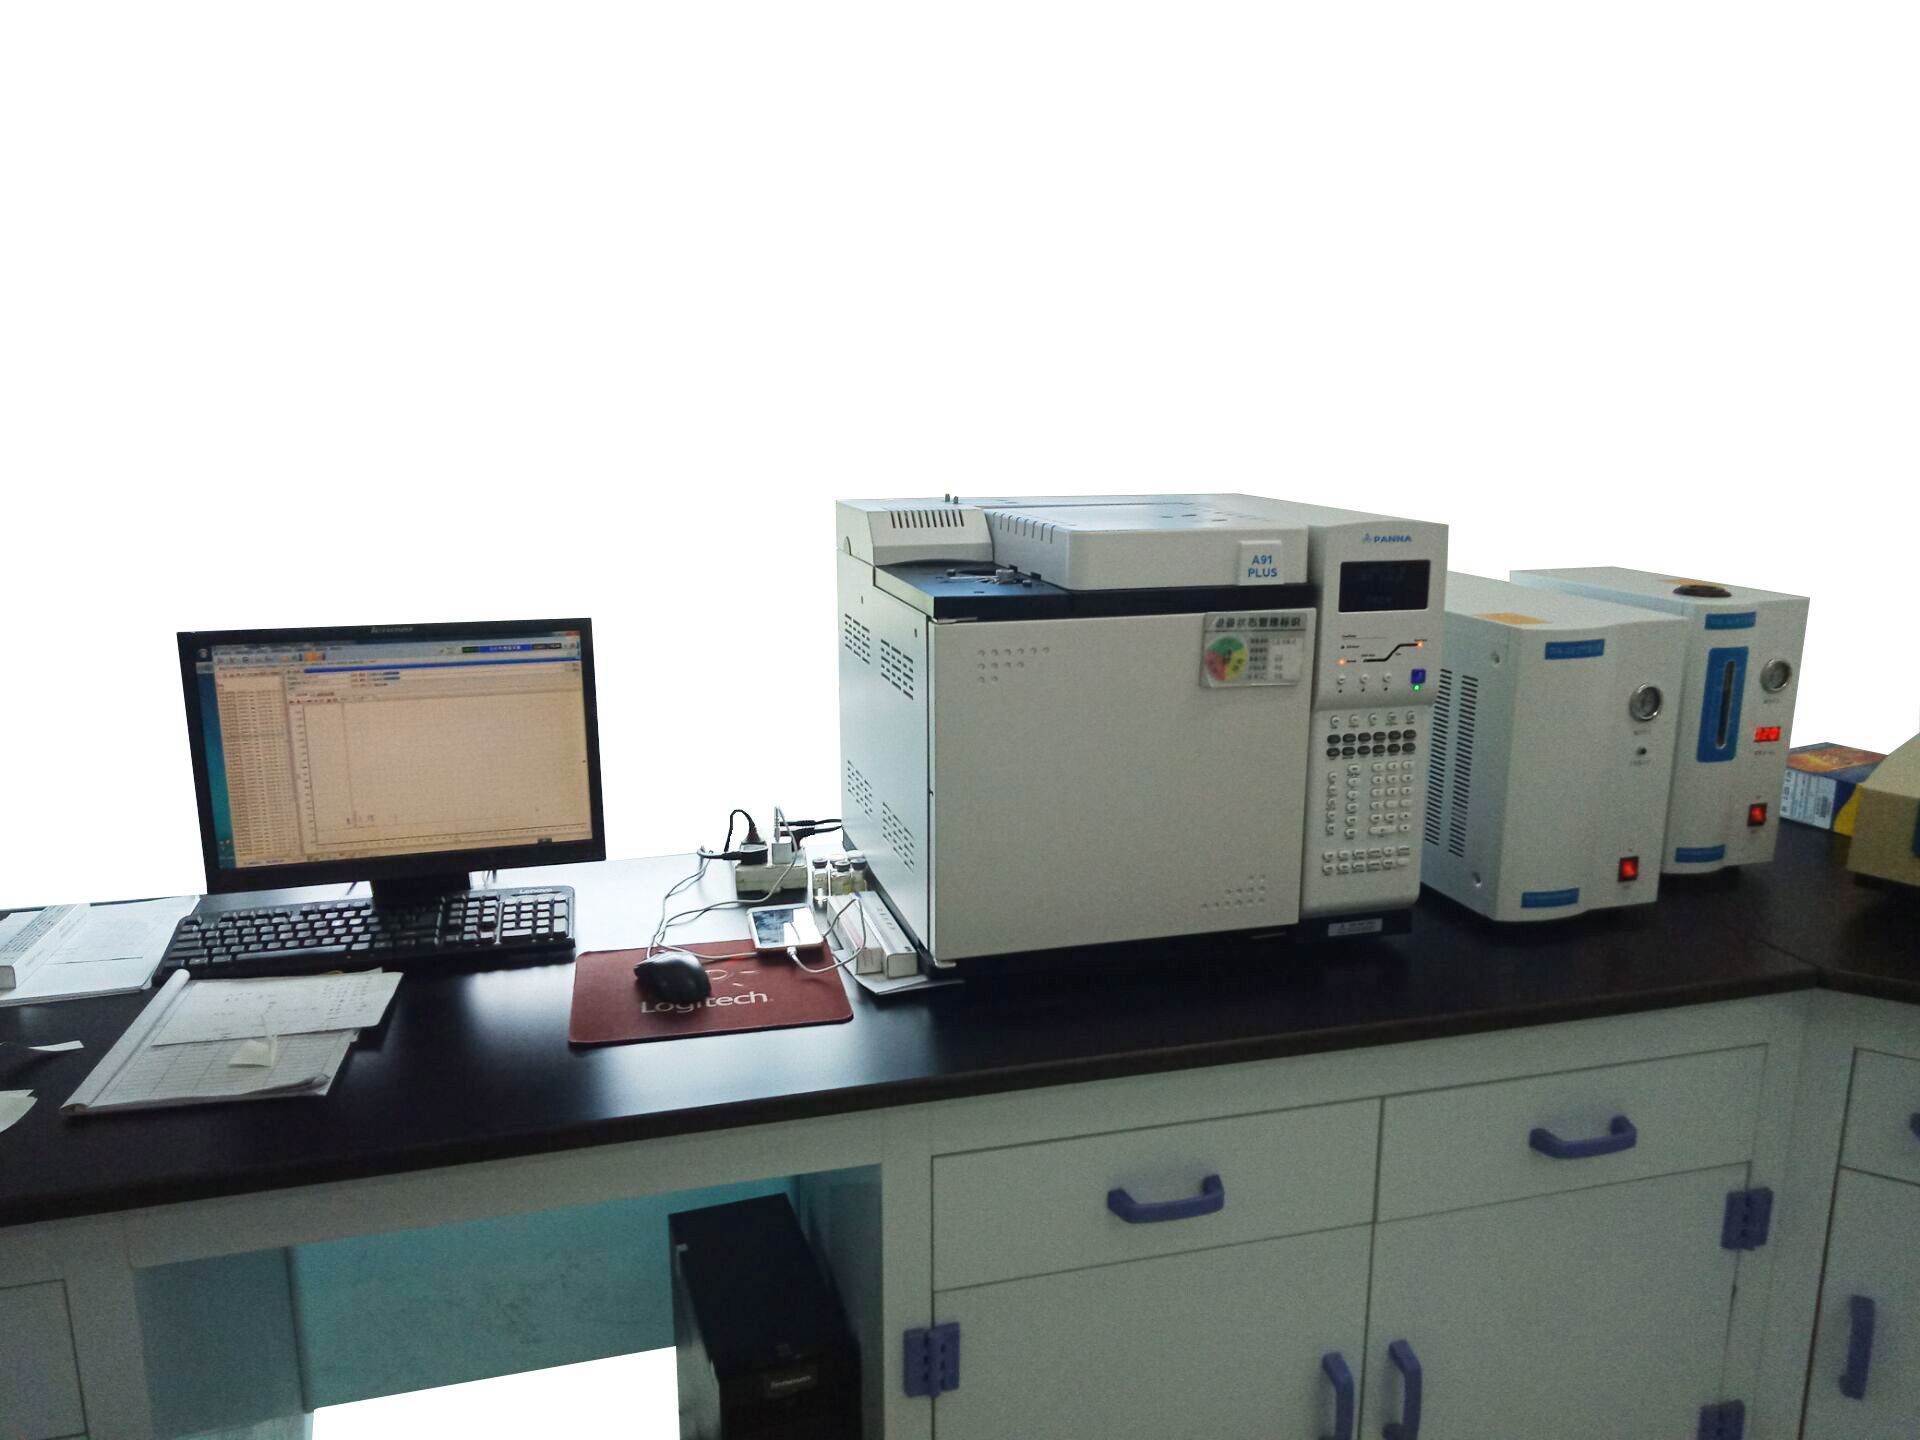
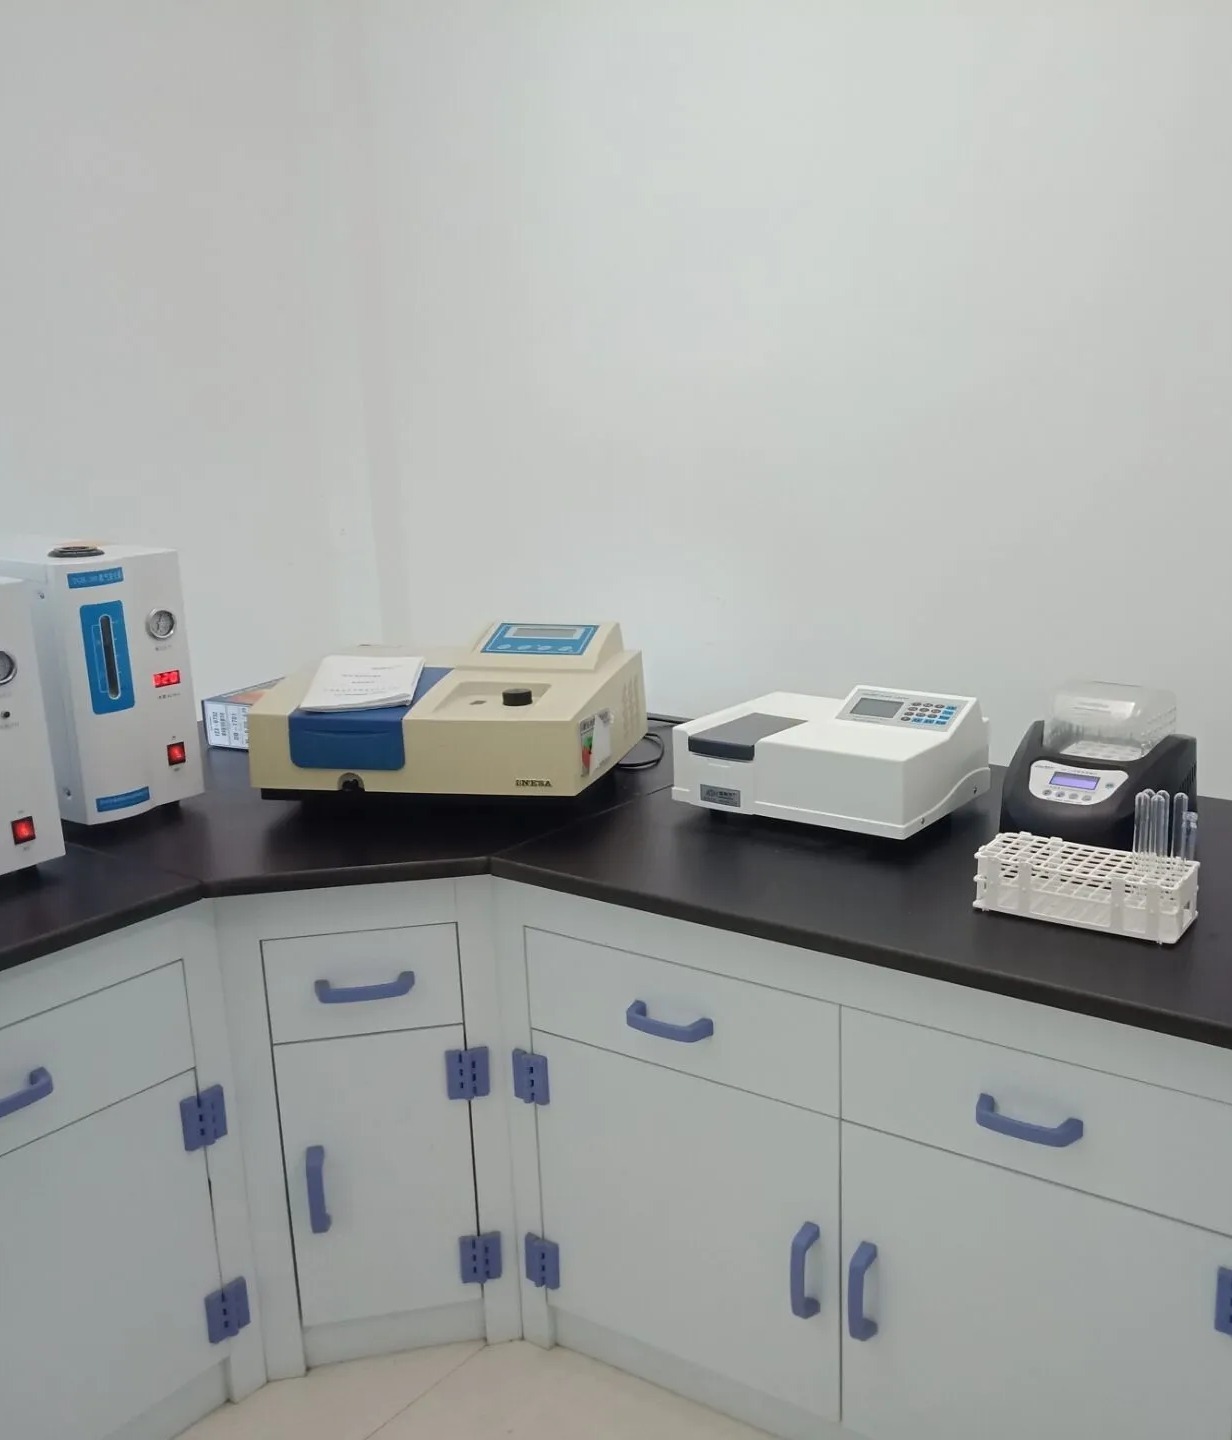
To guarantee superior, stable, and consistent product quality, we have established a comprehensive quality management system that covers every stage—from raw material receipt to final delivery. Our control procedures are built on a pharmaceutical-grade mindset, ensuring rigorous oversight at all times.
· IQC (Incoming Quality Control): All raw materials are strictly inspected against approved specifications, with suppliers regularly audited to ensure batch‑to‑batch purity and performance.
· IPQC (In‑process Quality Control): Critical parameters such as temperature, pressure, and reaction time are continuously monitored during production. Real‑time data recording allows immediate corrective actions if deviations occur.
· FQC (Final Quality Control): Finished products undergo comprehensive testing for physical and chemical properties, impurity profiles, and stability, using validated analytical methods.
· OQC (Outgoing Quality Control): Before shipping, each batch is re‑checked for labeling, packaging integrity, and compliance with customer requirements, ensuring that only conforming goods leave our facility.
· CAPA (Corrective and Preventive Action): Whenever any non‑conformance is identified, we initiate a root‑cause investigation and implement effective corrective measures. Preventive actions are then documented and fed back into the system to continuously upgrade our processes and eliminate recurrence.
Value Delivered
These integrated systems and rigorous practices enable us to deliver:
· Superior and consistent quality
· Stable supply
· Reasonable and competitive price
· Professional service from the whole team
· Social responsibilities
All these factors form the solid foundation for long‑term, mutually beneficial partnerships. With Mingxu, you choose not just a supplier, but a reliable quality partner.